 In high-throughput industrial environments—such as e-commerce fulfillment centers, chemical compounding bays, and food packaging lines—speed and repetitive handling efficiency dictate daily profitability. Operators at these sorting and palletizing stations routinely lift and move hundreds of corrugated cartons, wrapped boxes, and raw material sacks weighing between 25 kg and 65 kg during every single shift.
Under continuous rapid cycles, manual handling quickly violates global ergonomics standards like ISO 11228-1, causing physical operator strain and line deceleration. While automated robotics are costly, upgrading to engineered high-frequency vacuum tube lifters driven by centralized large-airflow air systems provides the ultimate cost-effective, high-yield solution for global B2B supply chains.
The Engineering Challenge of Porous Sacks and Taped Cartons
Implementing an efficient high-speed lifting line requires managing complex material surfaces. Traditional vacuum devices often fail when encountering two common industrial packaging formats:
- Sacks Exhibiting Continuous Sealing Decay: Raw material sacks made of woven polymers or thick paper packaging can loosen or sag slightly under load tension. This creates subtle micro-gaps that permit constant air leakage, causing low-volume lifters to instantly drop the item.
- Strapped and Taped Corrugated Cartons: Interlocking carton flaps, uneven tape seals, and plastic strapping bands break standard suction cup contact planes, triggering immediate vacuum loss.
To overcome these challenges without relying on slow mechanical clamps, a vacuum lifting system must be built with a massive airflow volumetric capacity capable of instantly overcoming surface micro-leakage.
Technical Performance: The Herolift VEL and HB400 Aerodynamics
Shanghai Herolift Automation Equipment Co., Ltd. resolves high-frequency handling bottlenecks by pairing the robust VEL Series lift tube infrastructure with the specialized HB400 high-volume industrial vacuum blower.
[System Blower Framework] -> Herolift HB400 Dry-Running Air Pump
[Volumetric Suction Rate] -> 320 m³/h (Driven via G3" Suction Port Connection)
[Motor Power Rating]      -> 5.5 kW (IE2 Energy Efficiency Rating / IP55 Enclosure)
[Net Equipment Weight]    -> 66 kg Frame Setup (73 dB Low-Noise Operation)
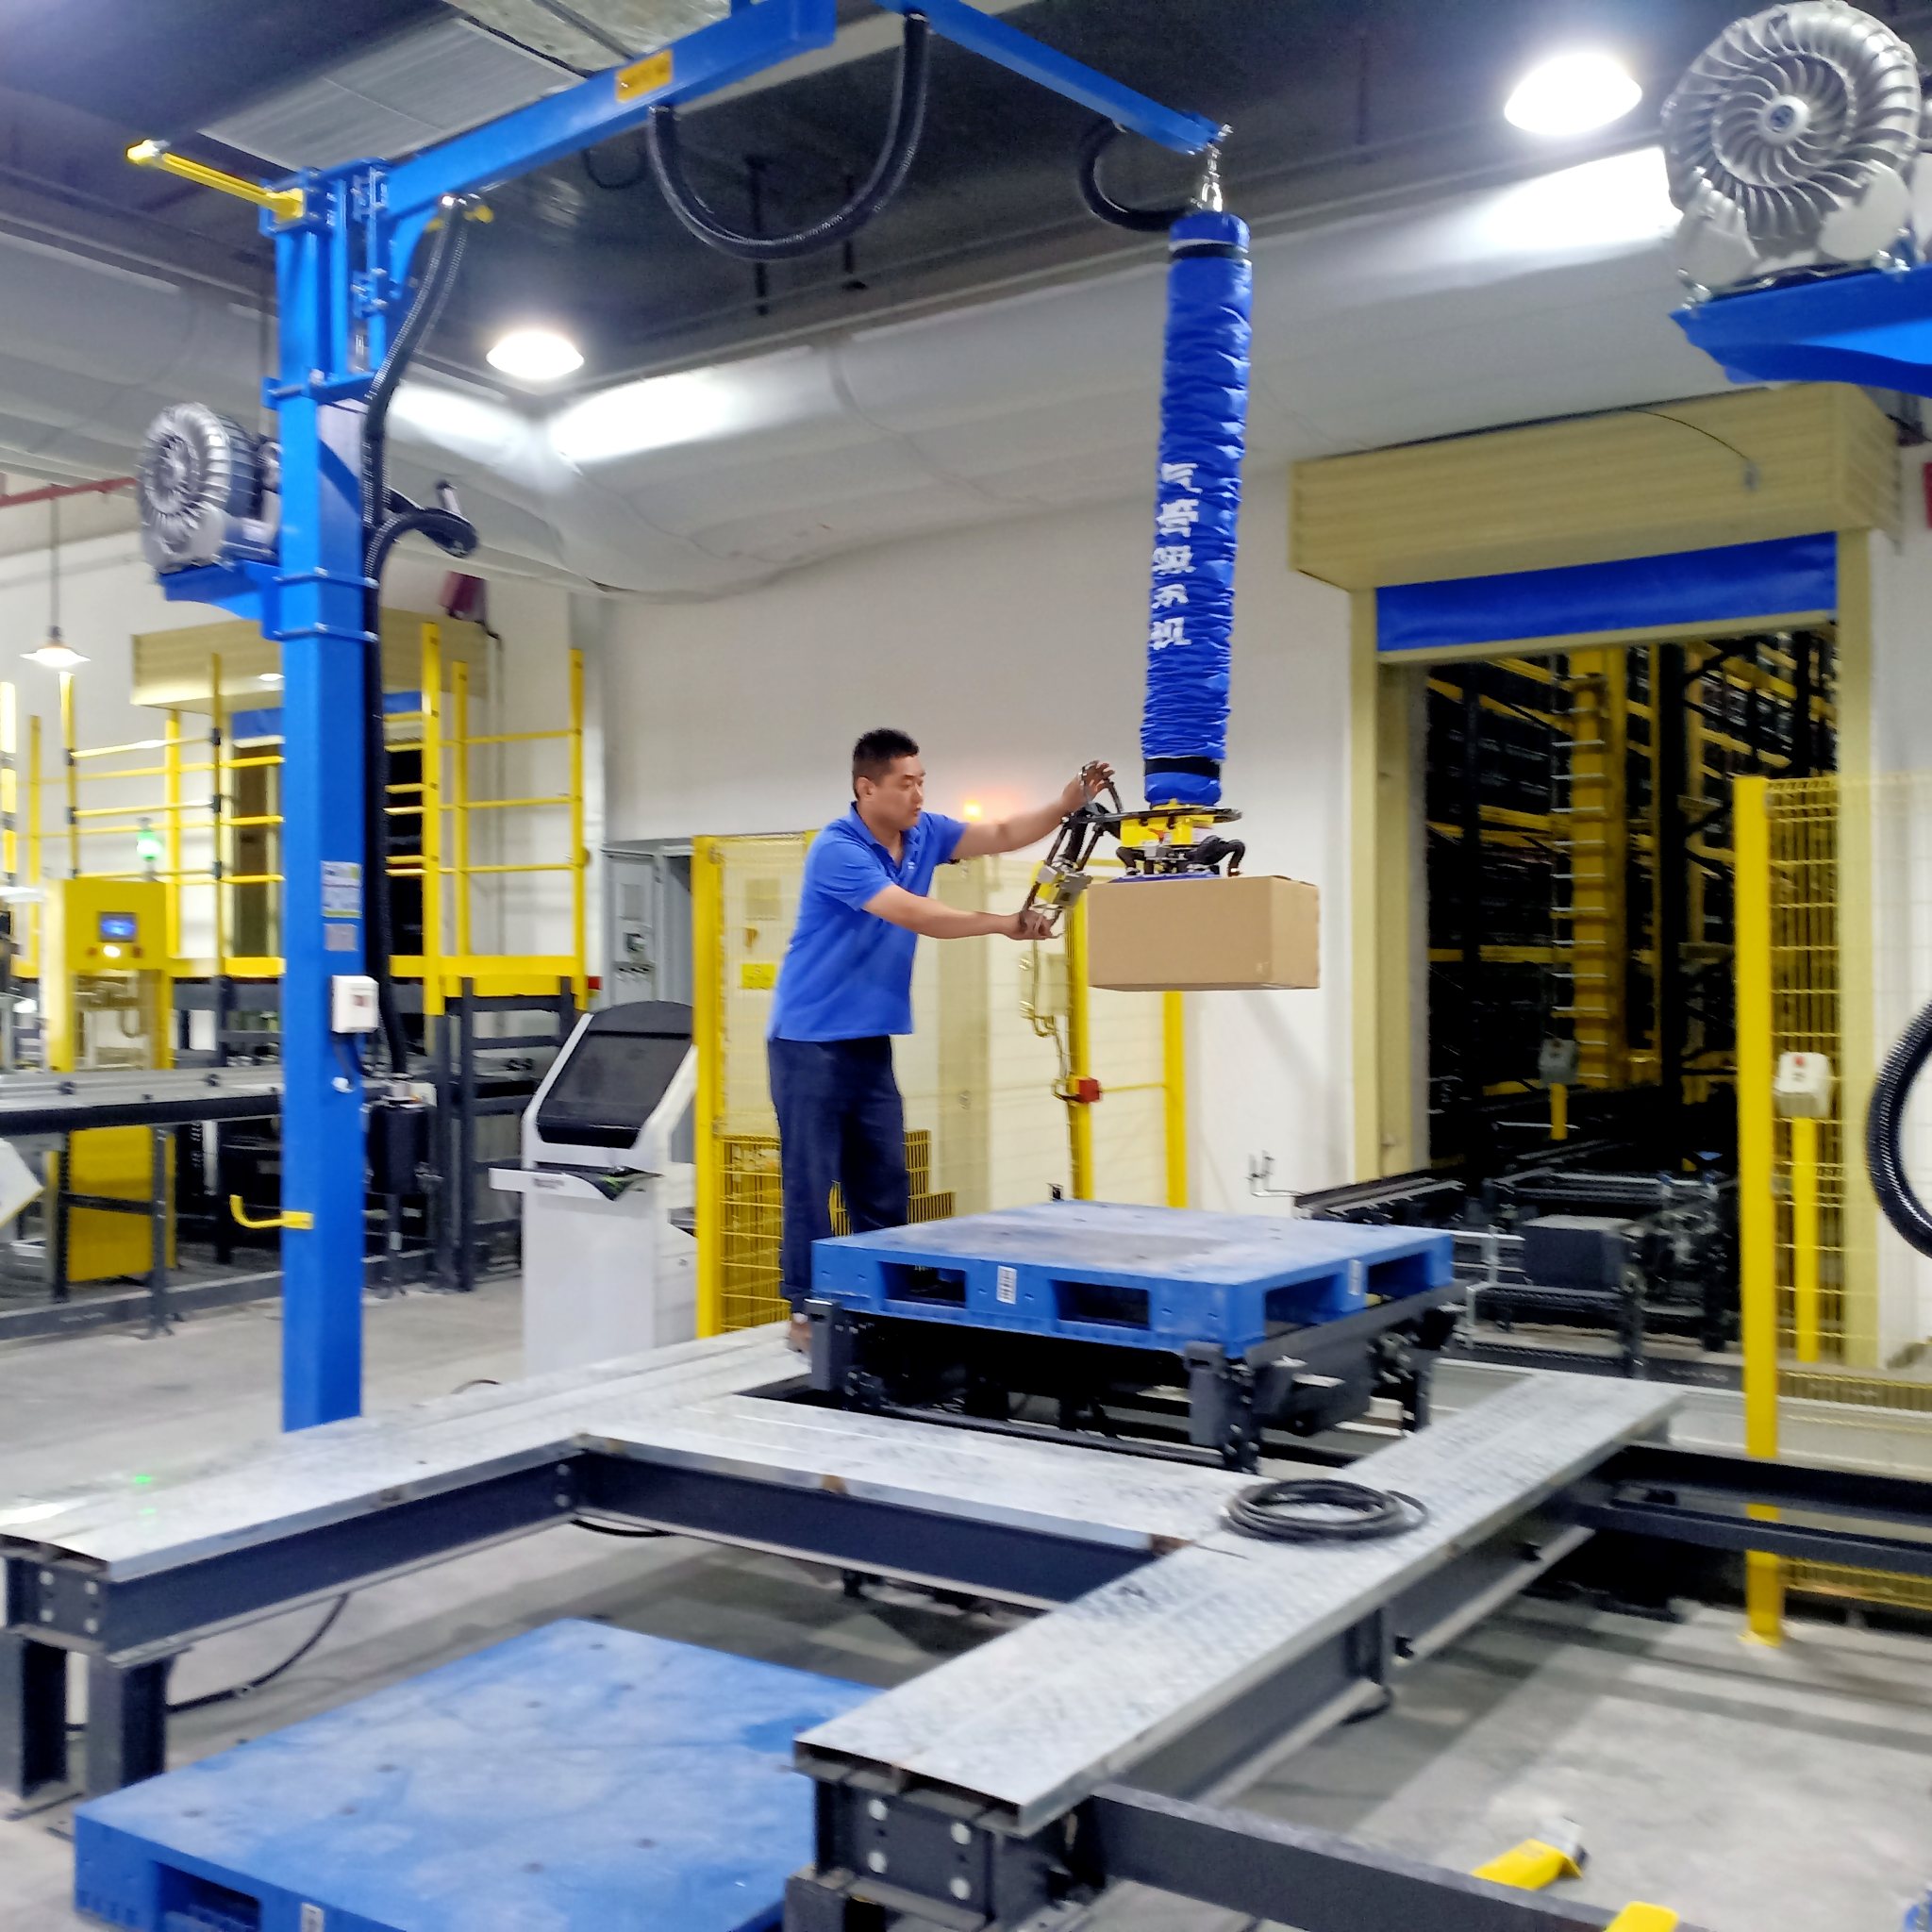
The core technical advantage of this platform centers on the HB400 Vacuum Blower, which delivers a high suction airflow rate of 320 m³/h through a heavy-duty G3″ suction connection. Driven by an energy-efficient 5.5 kW IE2 motor with IP55 ingress protection, this system maintains a steady vacuum flow even when pulling porous woven sacks or taped boxes with uneven tracking surfaces.
By sustaining high air-exchange volume rather than simple static pressure, the HB400 blower instantly compensates for incoming surface air leakage, ensuring the vacuum lifter tube retains complete physical control of the load during high-speed transit.
System Configurations for Rapid Handling Workstations
To precisely match the layout requirements of international logistics docks and compounding lines, Herolift configures the VEL system into distinct model pairings:
- VEL120 (Optimal 35–40 kg Loads): Utilizes a flexible 120 mm diameter lift tube designed for rapid single-handed order picking and fast carton stacking up to a maximum stack height of 2.4 meters.
- VEL140 (Optimal 50–65 kg Loads): Utilizes a heavy-duty 140 mm diameter lift tube matched for heavy chemical sacks, rubber blocks, and large raw sugar bags, allowing smooth lifting velocities of up to approximately 1 m/s.
- Intelligent Single-Hand Operation Control: The integrated control handle allows operators to seamlessly manage suction grip, variable vertical lift velocity, and full item release with one hand, converting tiring lifting movements into simple pushing and pulling gestures.
- Four-Foot and Sponge Pad Arrays: For strapped boxes or multi-sized carton arrays, Herolift integrates multi-point rectangular pads or durable NBR sponge seals that adjust to package variations without halting the conveyor line.
Strategic Price Advantage of Localized Engineering Integration
For global procurement managers evaluating material handling infrastructure, structural return-on-investment (ROI) is a primary consideration. European lifting brands often burden B2B buyers with high initial equipment costs and expensive proprietary replacement blowers.
By utilizing the fully integrated, mass-produced HB400 5.5kW blower platform, Herolift provides an exceptionally cost-effective alternative that matches European lifting performance while lowering spare part costs and initial capital expenses. This price-to-performance ratio ensures B2B facilities can deploy extensive, multi-station ergonomic lifter networks across expansive logistics grids without exceeding capital budgets.
Conclusion: Accelerate Your Logistics Output Safely
Eliminating manual strain while maximizing sorting throughput requires high-airflow vacuum lifting systems built for continuous heavy cycles. Backed by years of industrial manufacturing experience and international certifications including CE, ISO, and EAC, Shanghai Herolift transforms demanding manual packing areas into safe, high-efficiency production lines [source: 0.1.61].
Ready to calculate your factory floor cycle time savings? Explore our complete technical specifications and review active application case studies at hero-lift.com, or contact our applications team directly at
herolift@herolift.cn [source: 0.1.61].Post time: Oct-27-2026